Ready to Get Started?
Send us information on you, your company and your project. One of our experts will respond as soon as possible.
Direct Support: 0300 2799742 | info@fasttechinspection.com
Equipped with 10 multi-channel PWHT units (4 × 60 kW and 6 × 80 kW), ceramic heating elements, continuous calibrated chart recorders, and documented heating/soaking/cooling quality files.
PWHT applies an approved thermal cycle to welded components to relieve residual stresses, temper the metallurgical structure, and minimize brittle fracture risks. The job procedure strictly governs the heating band, thermocouple placement, heating rate, soak temperature and time, and controlled cooling.
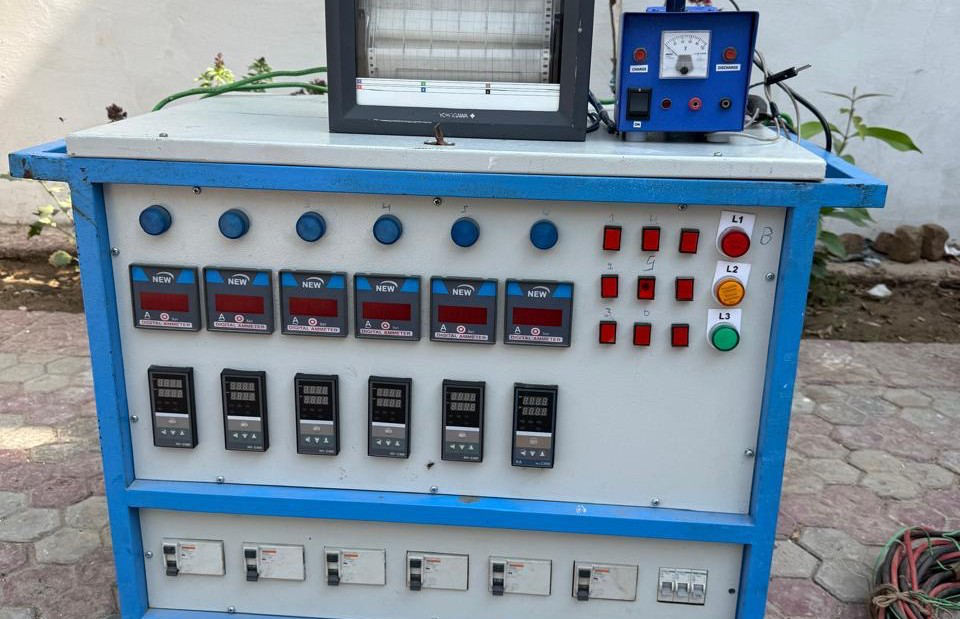
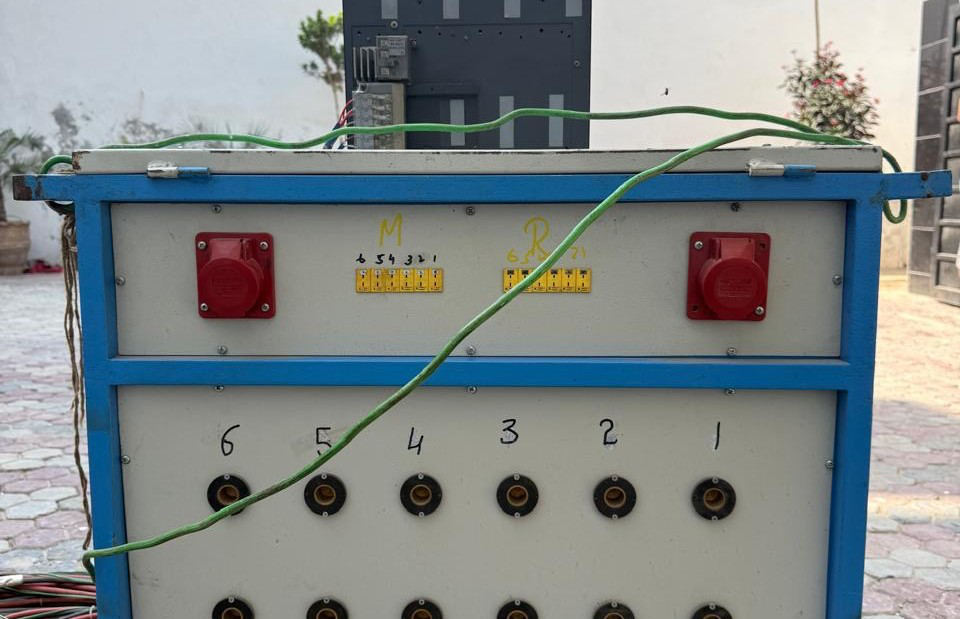
Fast Tech Inspection operates 4 units rated at 60 kW and 6 units rated at 80 kW. This substantial fleet allows us to mobilize rapidly across simultaneous high-capacity industrial projects.
Fast Tech Inspection rapid deployment teams are available 24 hours a day across Pakistan for emergency shutdowns, turnaround support, and critical NDT / PWHT requirements.
Call the 24/7 Field SupportSend us information on you, your company and your project. One of our experts will respond as soon as possible.
Direct Support: 0300 2799742 | info@fasttechinspection.com